


Reduced Tipping Costs. New Revenue. Paid Back in 12 Months.
How Sheffield Coated Stone Turned Returned Asphalt into Saleable Sub-Base with a REMU EP3150
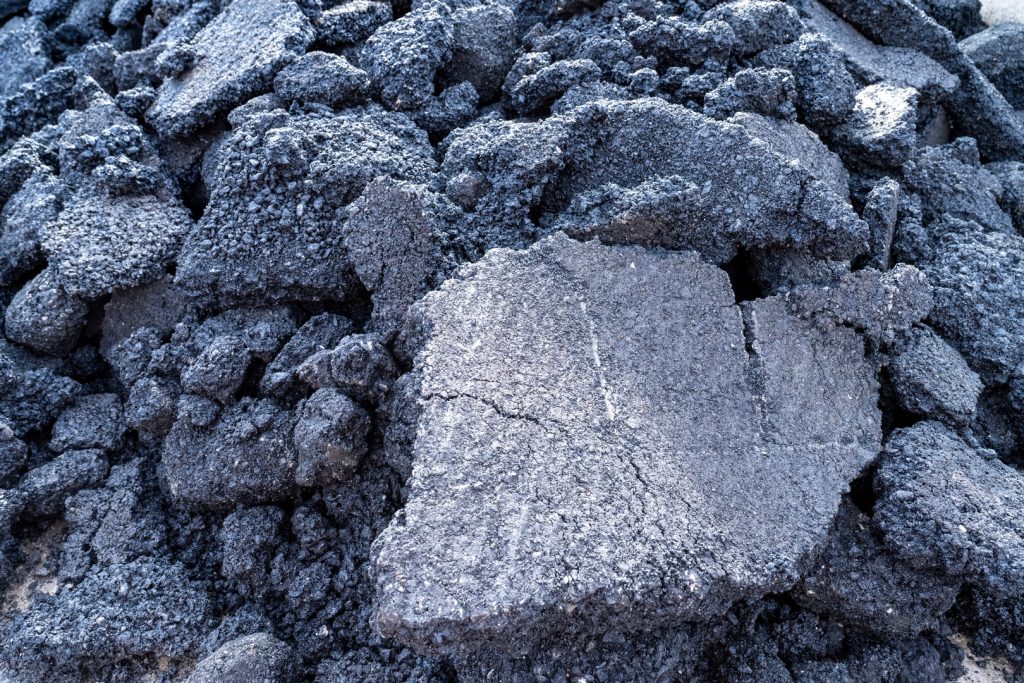
For John Corker, accepting returned asphalt has always been part of delivering great customer service. But while the approach helped customers, it also created a challenge for Sheffield Coated Stone. Returned material needed processing, and disposal costs were steadily mounting.
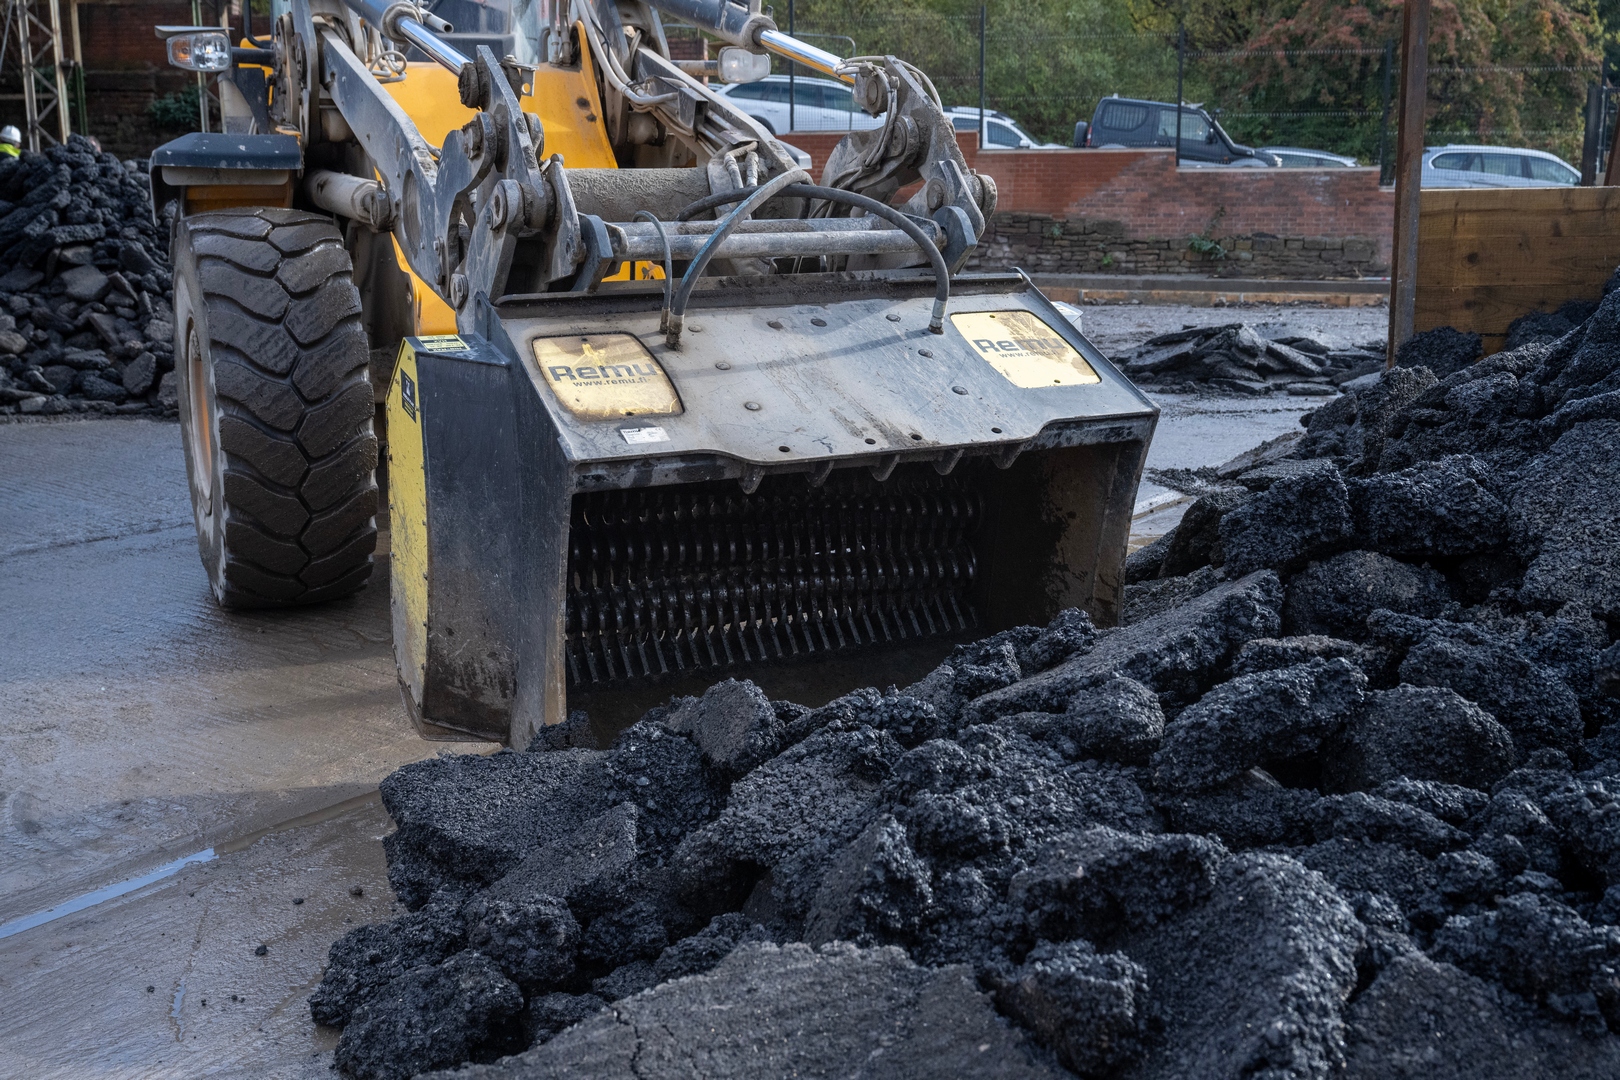
Working with Worsley Plant, the business invested in a REMU EP3150 screening bucket. The result was simple but effective: material that once cost money to dispose of became a saleable sub-base product.
The outcome? Lower tipping costs, a new revenue stream and a screening bucket that paid for itself within 12 months.

Aggregates
Aggregates
Aggregates
A Customer-Focused Asphalt Business
After a long career in the surfacing industry across South Yorkshire, John established Sheffield Coated Stone to fulfil his ambition of running his own asphalt plant.
Operating from its Rutland Street site, the business focuses on supplying asphalt to utility contractors, patching teams, builders, and developers. Customers can collect anything from a small Transit load through to a full eight-wheeler, with asphalt available from as early as 4am.
A key part of the company’s service is accepting unused material originally purchased from the plant, along with clean asphalt arisings from customers’ projects.
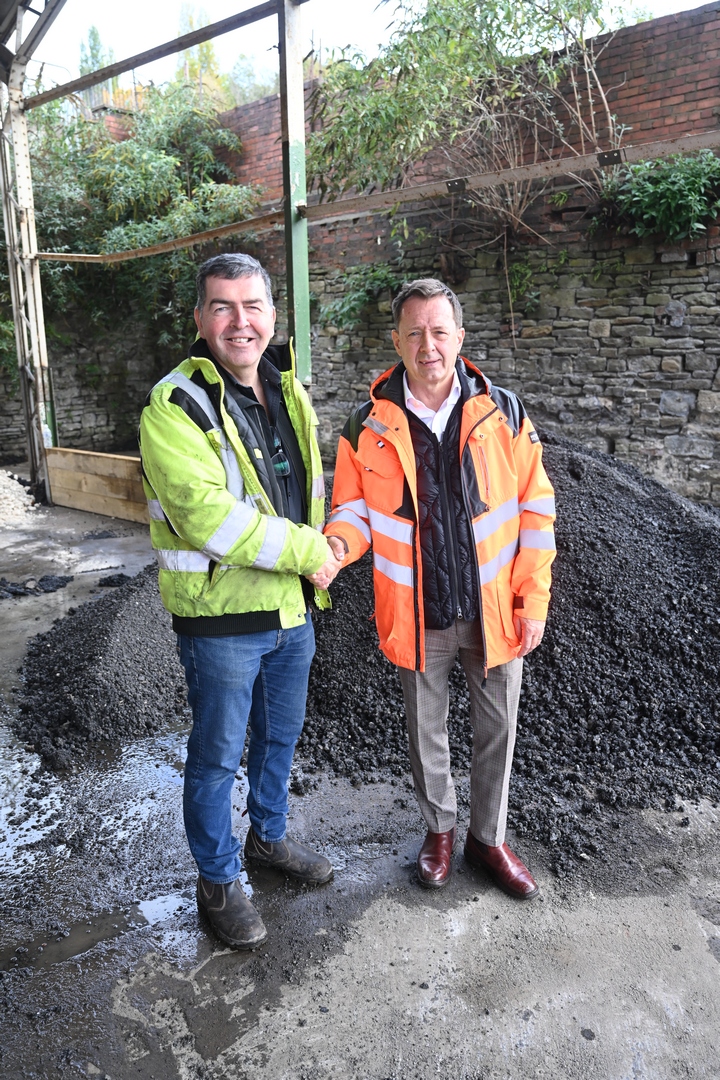
Turning a Disposal Cost into Revenue
While returned asphalt could be reintroduced into production, John wanted another outlet that maintained product quality while creating additional value for the business.
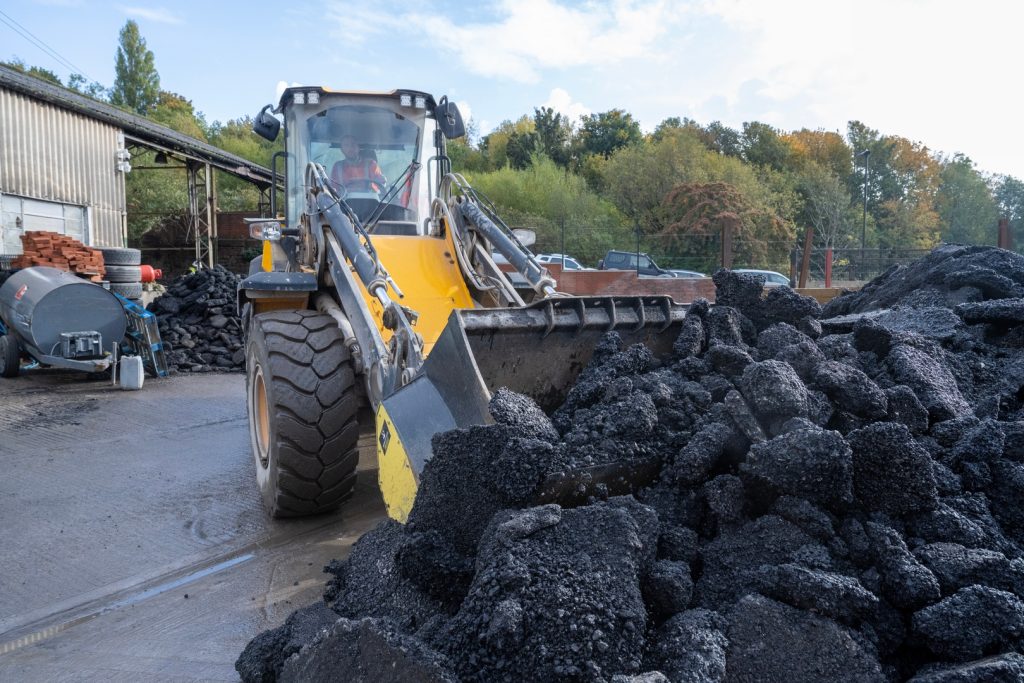
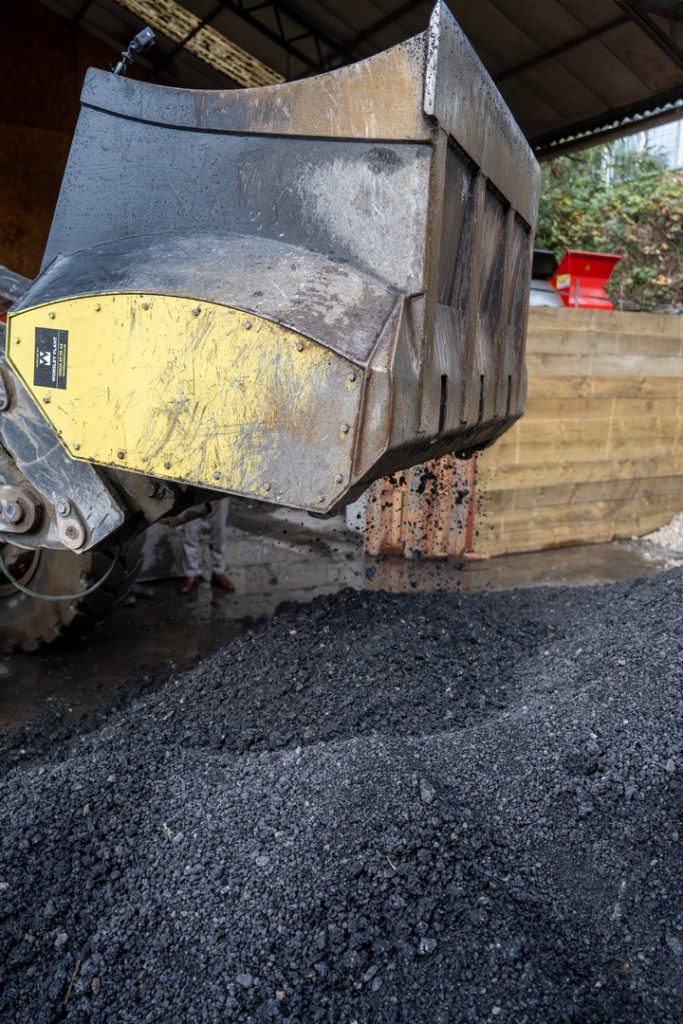
Working alongside Worsley Plant, he tested the material at the company’s Middlewich yard before selecting a REMU EP3150. A bespoke coupler was also supplied to suit the company’s JCB 437-wheel loader.
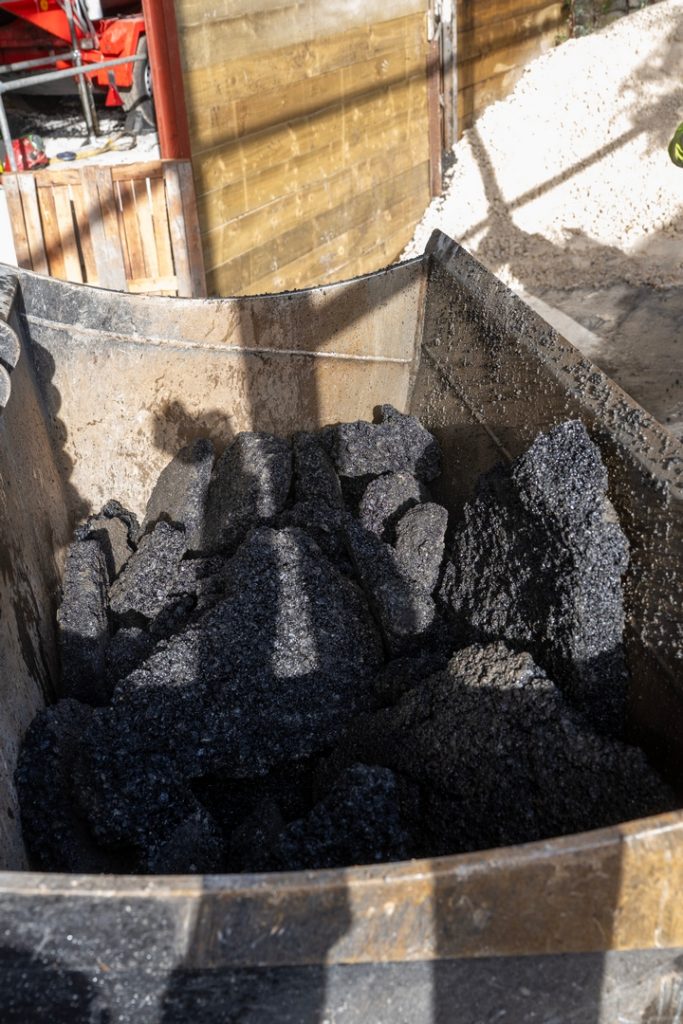
The testing process confirmed the REMU‘s shaft design could efficiently process the returned asphalt, producing a consistent product suitable for re-sale.
Creating a Product Customers Want to Buy
Initially, the processed material was marketed as recycled asphalt. However, John soon realised that description did not accurately reflect the finished product.
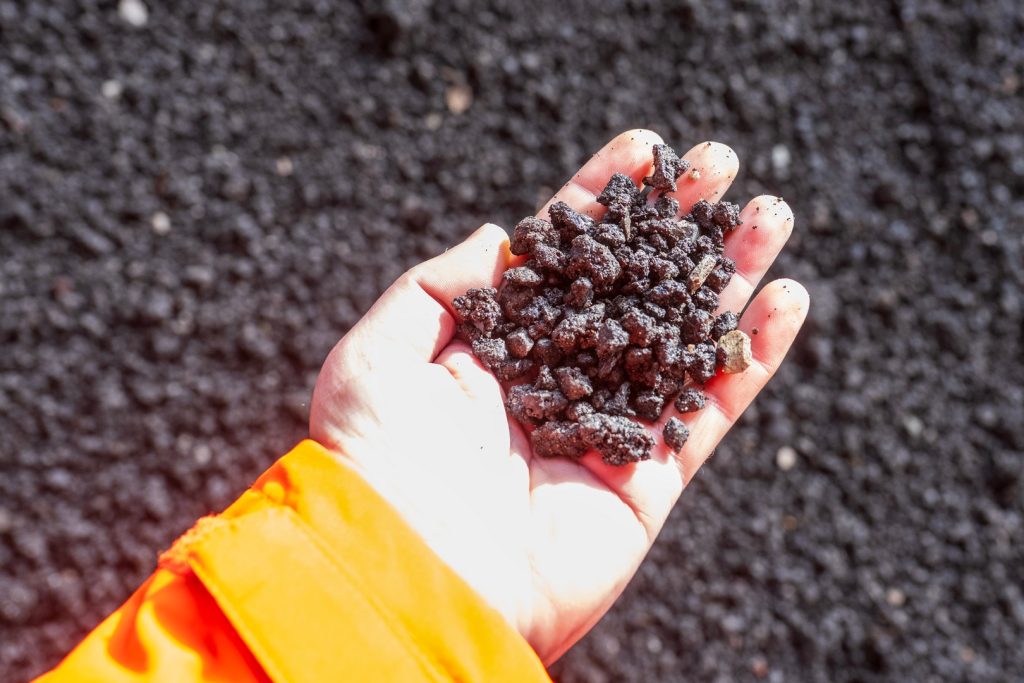
Rather than being a sticky black material, the screened product is more comparable to road planings: dry, clean, consistent, and ideal for use as sub-base.
It’s a perfect sub-base material, something our customers can’t get enough of.
By turning returned asphalt into a product customers actively wanted to purchase, Sheffield Coated Stone created a valuable new revenue stream while reducing the costs associated with disposal.
Recycling Around the Working Day
The recycling operation fits seamlessly around the plant’s day-to-day activities.
Returned material is left to cool and dry before being stockpiled. Once the morning rush of asphalt collections has finished for the day, a loader couples up to the REMU bucket and processes the material ready for re-sale.
This approach allows the business to utilise existing machinery and resources without impacting its primary operation.
An Investment That Paid Back Within 12 Months
With tipping costs ranging from £60 to £100 per tonne, disposing of returned asphalt can become a significant expense. Add transport costs and the financial impact soon mounts up.
By processing the material in-house, Sheffield Coated Stone benefits twice. The company spends less on disposal while generating income from the sale of processed sub-base material.
What was once a costly waste stream is now a profitable product line.
The combined savings and additional revenue meant the REMU EP3150 paid for itself within just 12 months.
Support for Future Growth
As demand for the recycled material continues to grow, John is already exploring additional attachments to further improve the process.
The relationship with Worsley Plant remains an important part of that development.
Conclusion
For Sheffield Coated Stone, the REMU EP3150 transformed returned asphalt from a disposal problem into a commercial opportunity.
By reducing tipping costs, creating a saleable sub-base product, and generating a new revenue stream, the business achieved full payback on its investment within the first year.
Call Worsley Plant on 01606 835 544 to find the right Remu Screening bucket for your setup.
You May Also be Interested in
Case Studies
MB Crusher
28 October 2026
One Man, One Machine, £1,500 Saved.
Read More

Case Studies
MB Crusher
7 January 2026
Building Efficiency: Duffin Builders Ltd’s Journey to Sustainable Construction with Innovative Equipment
Read More

Case Studies
Montabert
6 January 2026
Cardex’s Breaker Hit Its Limits On A Regeneration Project
Read More

DOWNLOAD THIS CASE STUDY